Every resin artist learns the same lesson at the same moment: the project is finished, the cure is complete, and the piece will not come out of the mold.
An epoxy resin release agent is what separates that moment from the one where the piece slides free exactly as intended. The right epoxy resin release agent, applied correctly to a properly cleaned mold, makes demolding so uneventful that it barely registers as a step in the process. An epoxy resin release agent that matches the mold material and the resin chemistry eliminates the struggle that beginners accept as normal. The wrong release agent, or none at all, turns demolding into a negotiation between the artist and the mold that the artist rarely wins.
The relationship between cleaning and release performance is not optional. A mold carrying residue from a previous pour will grip the next pour regardless of what epoxy resin release agent is applied. The epoxy resin release agent sits on top of whatever is already on the mold surface, which means every layer of old resin, dust, oil, or cured drips compromises the barrier. The epoxy resin release agent sits on top of whatever is already on the mold surface, not underneath it, which means every layer of old resin, dust, oil, or cured drips compromises the barrier between the piece and the mold.
This guide examines the eight most effective approaches to cleaning epoxy molds and selecting the right epoxy resin release agent for the material, the project, and the finish requirements. A release agent that is right for silicone is wrong for metal, and one that produces a matte finish will ruin a project requiring gloss. Each method addresses a specific mold type, contamination scenario, or release challenge that standard advice fails to handle.
Why Epoxy Resin Release Agent Performance Starts With Mold Preparation
The best epoxy resin release agent in the world cannot compensate for a mold that was not properly prepared to receive it. An epoxy resin release agent is only as effective as the surface it bonds to, and a contaminated surface guarantees a contaminated release.
Residue from previous pours acts as a bonding layer between old and new resin. Even a film invisible to the naked eye, oils from cured epoxy, dust settled from the air, mineral deposits from hard water drying, creates nucleation points where the new pour can mechanically grip the mold surface. The epoxy resin release agent applied over that residue bonds to the contamination rather than the mold, and the entire barrier fails at the weakest point.
Complete curing before demolding is the prerequisite to effective cleaning. Epoxy resin cures from the surface inward, and thick sections over half an inch may remain soft internally even when the exterior feels hard. Demolding before full cure leaves uncured resin on the mold that requires an epoxy resin release agent to overcome a contamination problem that patience would have prevented. Demolding before full cure not only risks damaging the piece but leaves uncured resin smeared across the mold surface, a contamination scenario that requires solvent cleaning rather than simple washing.
Environmental conditions during curing affect both the piece and the mold preparation for the next pour. Temperatures below sixty-five degrees Fahrenheit slow curing and can leave a tacky surface residue. Excessive heat causes uneven hardening that can trap release agent in surface irregularities. A consistent curing environment produces consistent release results. An epoxy resin release agent performs predictably when the curing conditions are predictable, and an epoxy resin release agent fails unpredictably when temperature and humidity vary from pour to pour.
The Soap and Water Method That Handles 90% of Mold Cleaning
Hot water and grease-cutting detergent solve more mold cleaning problems than any solvent. This method works without chemical damage risk, and it prepares the surface to receive an epoxy resin release agent with maximum adhesion. An epoxy resin release agent bonds best to a surface cleaned with hot water and soap, because that surface carries no solvent residue.
The process is simple but the details determine the result. Fill a container large enough to fully immerse the mold with water hot enough to be uncomfortable to the touch but not boiling. Boiling water can warp certain mold materials. Mix in a teaspoon of dish detergent, more for larger molds, until suds form throughout the solution. Immerse the mold completely and allow it to soak for thirty to sixty minutes. The detergent breaks down cured epoxy residue that is invisible to the eye but chemically active enough to grip the next pour. Removing this residue is what allows the epoxy resin release agent to form a continuous barrier rather than a patchy one.
After soaking, apply a few drops of detergent directly to the mold surface and scrub with a soft-bristle brush or non-abrasive sponge. Silicone molds require particular care: abrasive scrubbers create micro-scratches that trap resin in future pours, progressively degrading release performance even when an epoxy resin release agent is applied correctly. Work the brush into every corner, groove, and undercut, because these are the areas where residue concentrates and where the epoxy resin release agent must form its most reliable barrier.
Rinse thoroughly under running water. Soap residue left on the mold acts as a contaminant that interferes with the next application of epoxy resin release agent. An epoxy resin release agent applied over soap residue will fail at the points where the soap film prevents adhesion to the mold surface. Air-dry the mold completely, because moisture trapped in surface textures creates bubbles in the next pour and prevents the release agent from adhering uniformly. A lint-free microfiber cloth can accelerate drying in areas with hard water that would otherwise leave mineral deposits as the water evaporates.
This method handles the vast majority of mold cleaning scenarios. When it fails to remove visible residue or when the mold still feels tacky after drying, the contamination requires a solvent approach.
Isopropyl Alcohol: The Solvent That Dissolves What Soap Cannot
When cured epoxy residue resists soap and water, isopropyl alcohol at ninety-one percent concentration or higher dissolves the bond between the residue and the mold. This solvent cleans without damaging silicone or metal, preparing the surface for an epoxy resin release agent that must bond directly to the mold material.
The technique differs from the soap method in one critical respect: alcohol evaporates quickly, so the application must be immediate and thorough. Dampen a clean, lint-free cloth with the alcohol and rub firmly across the entire mold surface. The alcohol penetrates the residue, breaking the adhesion to the mold material. Continue rubbing until the cloth no longer picks up residue and the surface feels smooth rather than tacky under the cloth.
For tight corners, grooves, and undercuts, use a cotton swab saturated with alcohol to reach areas that the cloth cannot. These surfaces are where residue concentrates and where the epoxy resin release agent must perform most reliably. An epoxy resin release agent that covers every surface evenly is the goal, and cleaning every surface thoroughly is the prerequisite. Work the swab into the crevice, rotate to expose fresh swab surface as it picks up residue, and repeat until the swab emerges clean.
Allow the alcohol to evaporate completely before applying the epoxy resin release agent. Residual alcohol on the mold surface thins the release agent, creating an uneven barrier. An epoxy resin release agent applied to a surface still wet with solvent is an epoxy resin release agent that will fail at the thinnest points. The mold will feel cool as the alcohol evaporates and return to room temperature when dry. At that point, the surface is ready to receive an epoxy resin release agent that will bond directly to the mold material without any intervening contamination.
This method is effective on silicone and metal molds but should be tested on an inconspicuous area of plastic molds before full application. Some plastics, particularly acrylics and polycarbonates, can craze or cloud when exposed to high-concentration alcohol. For these materials, white vinegar provides a safer alternative that dissolves mineral deposits and light residue without the chemical aggression of alcohol.
The Freezer Method for Stubborn Resin That Cleaning Cannot Remove
When cured epoxy has bonded to the mold surface despite cleaning, the freezer method exploits the difference in thermal expansion between resin and mold material to break the adhesion mechanically rather than chemically.
Place the mold in a freezer for one to two hours. Epoxy resin contracts at a different rate than silicone or metal as it cools, and the differential expansion creates stress at the bond line that separates the materials. The resin becomes more brittle at low temperatures, making it easier to crack away from the mold surface in small pieces rather than stretching as it pulls.
Remove the mold from the freezer and immediately flex it gently. The bonded resin, now brittle, will crack and separate from the mold surface. Do not force pieces that resist. Return the mold to the freezer for additional time rather than applying force that could tear the mold material. Silicone molds are particularly vulnerable to tearing when cold because the material loses some of its natural elasticity at low temperatures.
After removing the brittle resin fragments, wash the mold with warm soapy water, dry thoroughly, and apply the epoxy resin release agent before the next pour. An epoxy resin release agent applied after freezer cleaning must cover a surface that has been thermally stressed, and thorough coverage compensates for any micro-cracks that the thermal cycle may have introduced. The thermal cycling does not harm silicone or metal molds but may affect certain plastics.
Test on an inconspicuous area before committing a valuable mold to the freezer. After thermal cleaning, the epoxy resin release agent must be applied to a mold that has returned to room temperature, because an epoxy resin release agent applied to a cold mold will not spread evenly.
How to Match the Right Epoxy Resin Release Agent to Silicone, Metal, and Plastic Molds
The release agent that performs flawlessly on silicone can destroy a metal mold’s finish. The epoxy resin release agent must match the mold material, the resin type, and the surface finish required. An epoxy resin release agent optimized for silicone will not serve a metal mold, and an epoxy resin release agent designed for high-detail casting will not suit a simple flat pour.
Silicone Molds: The Least Demanding but Still Requiring Preparation
Silicone molds possess natural non-stick properties that make them the most forgiving of all mold materials. New silicone molds benefit from a seasoning layer before first use. An epoxy resin release agent applied over a seasoned silicone surface performs better than one applied to raw silicone. This fills microscopic surface pores that can mechanically grip the first pour and establishes a baseline release surface that subsequent applications of epoxy resin release agent will maintain.
Silicone-compatible spray releases provide the most uniform coverage for complex shapes. An epoxy resin release agent in spray form reaches undercuts and detailed textures that brush-on products miss. Apply the epoxy resin release agent in thin, even coats from eight to ten inches, allowing ten to fifteen minutes of drying between each. Two to three thin coats outperform a single heavy application because the layers build a continuous barrier without the pooling that creates uneven release surfaces.
Avoid petroleum-based products on porous silicone. Petroleum jelly and mineral spirits degrade silicone over repeated exposure, and an epoxy resin release agent containing these compounds will shorten mold life. Water-based or silicone-based epoxy resin release agent formulations provide equivalent performance without the material damage. Water-based release agents or silicone-based sprays formulated specifically for mold release provide equivalent performance without the long-term material damage.
Metal Molds: The Wax-Dominated Territory
Metal molds require an epoxy resin release agent that forms a durable, uniform barrier. The higher pressures and tighter tolerances of rigid mold casting demand an epoxy resin release agent that will not compress, shift, or thin under load.
Carnauba wax-based paste releases are the standard epoxy resin release agent for metal mold work. Apply the epoxy resin release agent with a soft cloth using circular motions to work the wax into the surface. An epoxy resin release agent that penetrates rather than sits on top of the metal produces a release plane that epoxy cannot mechanically grip. Buff the excess away after five to ten minutes. The wax fills microscopic surface irregularities in the metal, creating a smooth release plane that epoxy cannot mechanically grip. Multiple thin coats produce better results than a single heavy application because the wax must penetrate the surface rather than sitting on top of it.
For high-detail metal molds, spray-on fluoropolymer releases such as 3M Novec provide an epoxy resin release agent that applies precisely without accumulating in tight geometries. An epoxy resin release agent that adds thickness to fine features degrades cast quality, and fluoropolymer sprays add the least thickness of any release method. These releases are more expensive than wax alternatives but pay for themselves in mold longevity and reduced cleaning requirements between pours.
Plastic Molds: Where Chemical Compatibility Determines Success
Plastic molds present the most challenging release scenario. The epoxy resin release agent must prevent adhesion without chemically interacting with the mold, and an epoxy resin release agent that is safe on silicone can craze or cloud certain plastics on contact.
Water-based release agents eliminate the solvent damage risk that alcohol or petroleum products pose to many plastics. An epoxy resin release agent formulated for plastic molds avoids the chemical interactions that cloud clear plastic or etch polished surfaces. Apply the epoxy resin release agent with a foam brush to avoid the streaking that bristle brushes leave on visible surfaces. The foam distributes the release agent evenly without the brush marks that transfer to the final piece.
Test any epoxy resin release agent on an inconspicuous area of the plastic mold before full application. Some plastics react with chemicals that are inert on silicone or metal, and the reaction may not be immediately visible. An epoxy resin release agent that passes a twenty-four-hour patch test on the specific plastic being used can be applied with confidence. A twenty-four-hour test patch reveals compatibility issues that would otherwise be discovered when the cured piece emerges with surface defects. An epoxy resin release agent that fails a patch test saves the mold. An epoxy resin release agent that is never tested risks the entire project.
The Multi-Coat Philosophy That Transforms Release Performance
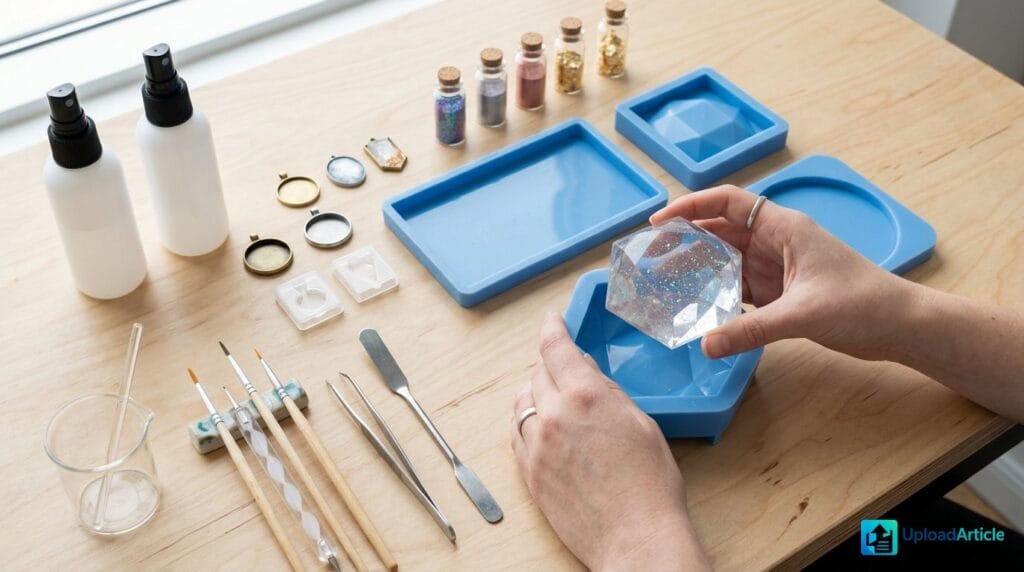
The single most common mistake with any epoxy resin release agent is applying one heavy coat instead of multiple thin coats. An epoxy resin release agent applied in a single heavy layer pools, streaks, and dries unevenly.
A heavy coat pools in low areas, streaks across high areas, and dries with varying thickness that creates an uneven release surface. The thin areas fail first, and once the epoxy bonds to the mold at any point, that bond becomes a focal point for stress that propagates across the entire release plane.
Two to three thin coats of epoxy resin release agent build a continuous barrier of uniform thickness. The first coat fills microscopic surface irregularities. The second coat establishes the continuous release plane. The third coat provides the safety margin that prevents localized bonding. The first coat fills the microscopic surface irregularities of the mold. The second coat establishes the continuous release plane. The third coat, when the mold geometry justifies it, provides the margin of safety that prevents the kind of localized bonding that ruins both the piece and the mold.
Each coat requires ten to fifteen minutes of drying time. Rushing the process creates a composite layer weaker than either coat applied individually. The solvents in the fresh epoxy resin release agent partially dissolve the previous layer before it has set, and an epoxy resin release agent that is rushed produces worse results than one applied with patience.
The Cleaning Sequence Between Pours That Extends Mold Life
The cleaning discipline between pours determines mold longevity more than any other variable. An epoxy resin release agent performs exactly as well as the surface it is applied to, and a surface that is cleaned after every pour produces consistent release results. A mold that is cleaned properly after every use will survive hundreds of pours. A mold that accumulates residue over multiple uses will develop bonding problems that require increasingly aggressive cleaning, eventually damaging the mold surface beyond recovery.
The sequence is straightforward. Demold the piece. Inspect the mold under bright light for visible residue, paying particular attention to corners and undercuts. If residue is visible, proceed to the isopropyl alcohol method. If the mold appears clean, wash with warm soapy water as described in the first cleaning method regardless. The invisible residue that looks clean under ambient light will grip the next pour, and the five minutes invested in washing costs far less than the hour spent repairing a piece that tore during demolding.
Dry the mold completely. Apply the epoxy resin release agent in thin, even coats. Allow the final coat to dry completely before pouring. An epoxy resin release agent applied to a properly cleaned and dried mold produces the predictable release that makes demolding uneventful. The mold is now prepared for the next pour with a clean surface and a fresh epoxy resin release agent barrier. An epoxy resin release agent applied to a mold that has been cleaned and dried according to this sequence will produce predictable, repeatable results.
Molds cleaned and prepared according to this sequence between every pour will outperform molds cleaned only when visible contamination appears. The variable in this equation is not the release agent. The cleaning discipline is, and even the best epoxy resin release agent can only compensate so much for a surface that was never properly prepared. The discipline feels excessive until the first time a piece releases perfectly after a cleaning cycle that would have been skipped under a less rigorous standard.
The Solvent Hierarchy: What to Reach for When Soap Fails
When hot soapy water fails to remove residue, the solvent choice depends on the mold material and the contamination type.
Isopropyl alcohol at ninety-one percent or higher is the first solvent for silicone and metal molds. It dissolves cured epoxy residue without damaging the surface, and it leaves no residue that would interfere with the epoxy resin release agent applied afterward. An epoxy resin release agent applied to a surface cleaned with alcohol bonds better than one applied to a surface cleaned with water alone. For plastic molds, white vinegar provides a safer alternative that removes mineral deposits and light organic residue without the chemical aggression of alcohol.
Acetone removes cured epoxy more aggressively than alcohol but damages many plastics and can degrade silicone over repeated exposure. Reserve acetone for metal molds only, and test on an inconspicuous area before full application. Acetone strips every trace of previous epoxy resin release agent along with the contamination, requiring complete reapplication. An epoxy resin release agent applied after acetone cleaning must cover a surface that has been chemically stripped to bare material. The acetone will strip every trace of previous release agent along with the contamination. An epoxy resin release agent must be completely reapplied after acetone cleaning because the solvent removes the old release barrier as thoroughly as it removes the contamination.
For the most stubborn contamination, a commercial resin cleaner formulated for epoxy removal provides targeted chemistry that generic solvents cannot match. After using the cleaner, wash with soap and water before applying the epoxy resin release agent. An epoxy resin release agent applied over cleaner residue will not bond to the mold surface. Apply according to manufacturer instructions, typically involving a dwell time of several minutes to soften the bond before wiping away, and follow with a soap and water wash to remove cleaner residue before applying fresh release agent.
The solvent hierarchy exists because aggression correlates with risk. The mildest effective solvent is always correct. An epoxy resin release agent can only perform as well as the mold surface it is applied to, and a mold surface damaged by unnecessarily aggressive cleaning will never release as cleanly as one maintained with restraint. An epoxy resin release agent can only perform as well as the mold surface it is applied to, and a mold surface damaged by unnecessarily aggressive cleaning will never release as cleanly as one maintained with restraint.
Frequently Asked Questions
What is the best epoxy resin release agent for silicone molds?
Silicone-compatible spray releases provide the most uniform coverage for silicone molds, applied in two to three thin coats with complete drying between each. New silicone molds benefit from a seasoning layer of food-grade mineral oil buffed dry before the first use.
Can I use household products as an epoxy resin release agent?
Petroleum jelly diluted with mineral spirits creates a functional release agent for small projects. Cooking sprays work in a pinch. But these household alternatives produce inconsistent results compared to a purpose-formulated epoxy resin release agent. An epoxy resin release agent engineered for mold release will always outperform improvised substitutes.
How do I clean cured epoxy resin from a mold that will not release?
The freezer method exploits thermal expansion differences: place the mold in a freezer for one to two hours, then flex gently to crack the brittle, cold resin away from the mold surface. Repeat as needed rather than applying force that could tear the mold.
How many coats of epoxy resin release agent should I apply?
Two to three thin coats outperform one heavy coat. Each coat requires ten to fifteen minutes of drying time. The multiple thin layers build a continuous, uniform barrier that a single heavy application cannot achieve because it pools and streaks across the mold surface.
Does isopropyl alcohol damage silicone molds?
Isopropyl alcohol at ninety-one percent or higher is safe for silicone and metal molds when used to dissolve cured epoxy residue. Test on plastic molds before full application because some plastics craze or cloud when exposed to high-concentration alcohol.
How often should I clean my resin molds?
Clean molds after every pour regardless of whether visible residue is present. The invisible residue that appears clean under ambient light will grip the next pour, and five minutes of cleaning between every use costs far less than repairing a torn piece or replacing a damaged mold.
Conclusion
The difference between a piece that demolds perfectly and one that tears, sticks, or destroys the mold is almost never luck. It is cleaning discipline and epoxy resin release agent selection, applied consistently. An epoxy resin release agent chosen for the specific mold material and resin chemistry, applied to a mold cleaned after every pour, produces results that look effortless but required discipline to achieve.
An epoxy resin release agent performs exactly as well as the mold surface it is applied to. Cleaning that surface after every pour, using the mildest effective method, and applying the epoxy resin release agent in multiple thin coats rather than a single heavy application, produces the reliable release that makes demolding forgettable. The epoxy resin release agent is not the variable. The preparation is. The mold that receives this treatment will outlast molds that are cleaned only when visible contamination demands it, and the pieces it produces will reflect the care invested in preparation.
The methods described in this guide cover the full range of mold materials, contamination types, and release challenges. An epoxy resin release agent matched to the mold material, applied in multiple thin coats to a thoroughly cleaned surface, will produce the release performance that makes demolding the easiest step in the project. The sequence is not complicated: clean, dry, apply epoxy resin release agent, dry, pour, repeat. An epoxy resin release agent applied according to this sequence will produce consistent results across hundreds of pours. An epoxy resin release agent applied to a contaminated surface will fail regardless of its quality or price.